
 Image 1 of 1
Materials
ABS (Acrylonitrile Butadiene Styrene): Lightweight, impact-resistant, dimensionally stable, and fully compatible with decorative electroplating surface treatment — the standard substrate for premium decorative hardware and consumer electronics exterior components
Surface Finish — Brushed Nickel Electroplating
Multi-layer electroplating: copper base coat for surface levelling + semi-bright nickel for corrosion resistance + bright nickel for reflectivity + satin nickel top coat
Brushed nickel finish: directional linear brush texture applied uniformly across all exterior faces prior to final sealing — producing a consistent warm satin metallic sheen
Resistant to UV exposure, humidity, and daily contact wear under normal indoor use conditions
Key Advantages
Single-Piece CNC-Machined Construction — The complete perimeter frame is machined from a single billet of aluminium alloy with no weld joints, parting lines, or assembly seams on any exterior surface — delivering the structural integrity, dimensional accuracy, and seamless aesthetic of flagship OEM smartphone hardware.
Permanent Hard Anodised Surface — Hard anodising converts the aluminium surface into a dense oxide layer chemically bonded to the substrate — providing scratch, abrasion, and corrosion resistance that no paint, PVD, or electroplated coating can match for a device carried daily in pockets and bags.
Precise Button & Port Geometry — CNC-machined button cutouts, port apertures, and perforation arrays are held to tight dimensional tolerances, ensuring correct OEM button travel, charging port connector alignment, and acoustic performance from the speaker grille array.
Space Grey Premium Positioning — The controlled anodise dye process produces a consistent, repeatable space grey colour across production batches — matching the restrained, premium hardware aesthetic of leading flagship smartphone product lines.
High Strength-to-Weight — 6061-T6 or 7075-T6 aluminium alloy delivers the structural rigidity required to protect internal device components from flex, drop impact loading, and torsional stress at a frame weight of approximately 22 g — significantly lighter than stainless steel frame alternatives.
Full OEM Customization — All dimensional, geometric, layout, and surface finish parameters can be specified to match exact smartphone model design requirements, including model-specific button positions, port formats, and antenna break geometry.
Key Features
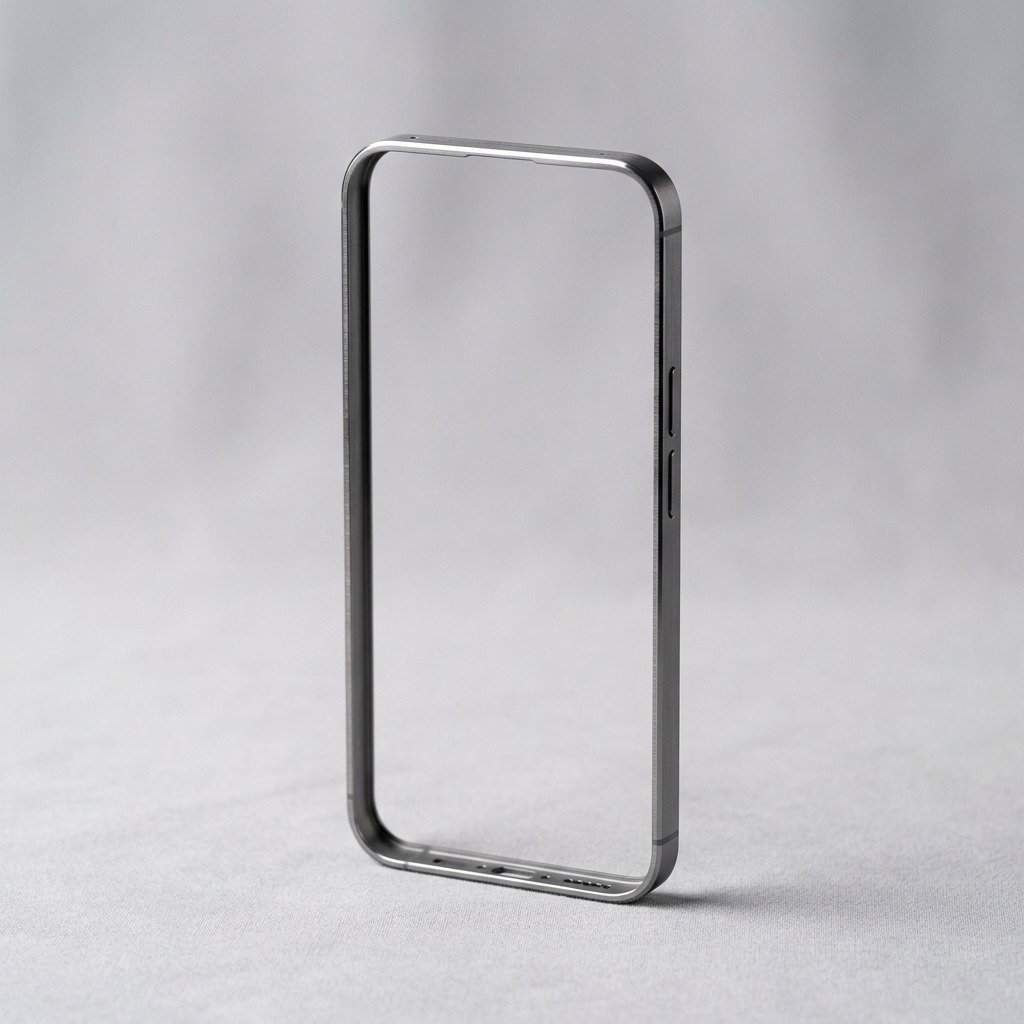
Single-piece CNC-machined aluminium alloy perimeter frame — no exterior weld joints or seams
Generously radiused corners — approx. R18 mm for premium ergonomic grip profile
Right rail: precision-machined volume up, volume down, and power button cutouts
Bottom rail: USB-C port aperture, speaker grille perforation array, microphone port
Left rail: SIM card tray slot with machined tray guide geometry
Fine directional brushed satin texture across all exterior rail faces
Hard space grey anodised finish — approx. 15 – 20 μm oxide layer, permanently bonded
Deburred and chamfered all cutout edges for smooth tactile contact
Aluminium Alloy 6061-T6 (standard) / 7075-T6 (high-strength OEM option)
Weight: approx. 22 g
Full OEM dimension, layout, and finish customization available
Manufacturing Process
Billet Preparation — Aluminium alloy 6061-T6 or 7075-T6 billet is cut to stock size for individual frame machining, ensuring consistent alloy grain structure and material properties throughout every frame component.
CNC Roughing — Multi-axis CNC machining removes the majority of billet material to produce the approximate frame perimeter geometry, internal cavity, and primary feature positions in a first-operation roughing pass.
CNC Finishing — High-precision finishing passes machine the exterior rail faces, corner radii, button cutouts, port apertures, speaker grille perforation array, SIM tray slot, and internal assembly fit surfaces to final dimensional tolerances.
Deburring & Edge Treatment — All machined cutout edges, perforation arrays, and rail edges are deburred, chamfered, and hand-finished to remove sharp edges and ensure smooth tactile feel at all finger contact points.
Mechanical Brushing — Fine directional linear brush texture is applied uniformly across all exterior rail faces using controlled abrasive tooling, producing a consistent fine satin grain across the full frame perimeter.
Pre-Anodise Cleaning — Parts undergo multi-stage alkaline cleaning, acid etching, and deoxidising to prepare a chemically clean aluminium surface for uniform anodise penetration and colour consistency.
Hard Anodising & Colouring — Parts are anodised in a controlled sulphuric acid bath to grow a 15 – 20 μm oxide layer, then immersed in space grey anodise dye solution for colour penetration before hot sealing.
CMM Dimensional Inspection — Critical dimensions including overall frame size, corner radius, button cutout positions, port aperture geometry, and internal assembly fit surfaces are verified on coordinate measuring equipment before shipment.